How to Weld Stainless Steel: Filler, Gas and Heat Control
Stainless steel welds with TIG, MIG or stick if you match the filler, use the right gas and keep heat low. Covers grades, sugaring and fume safety.
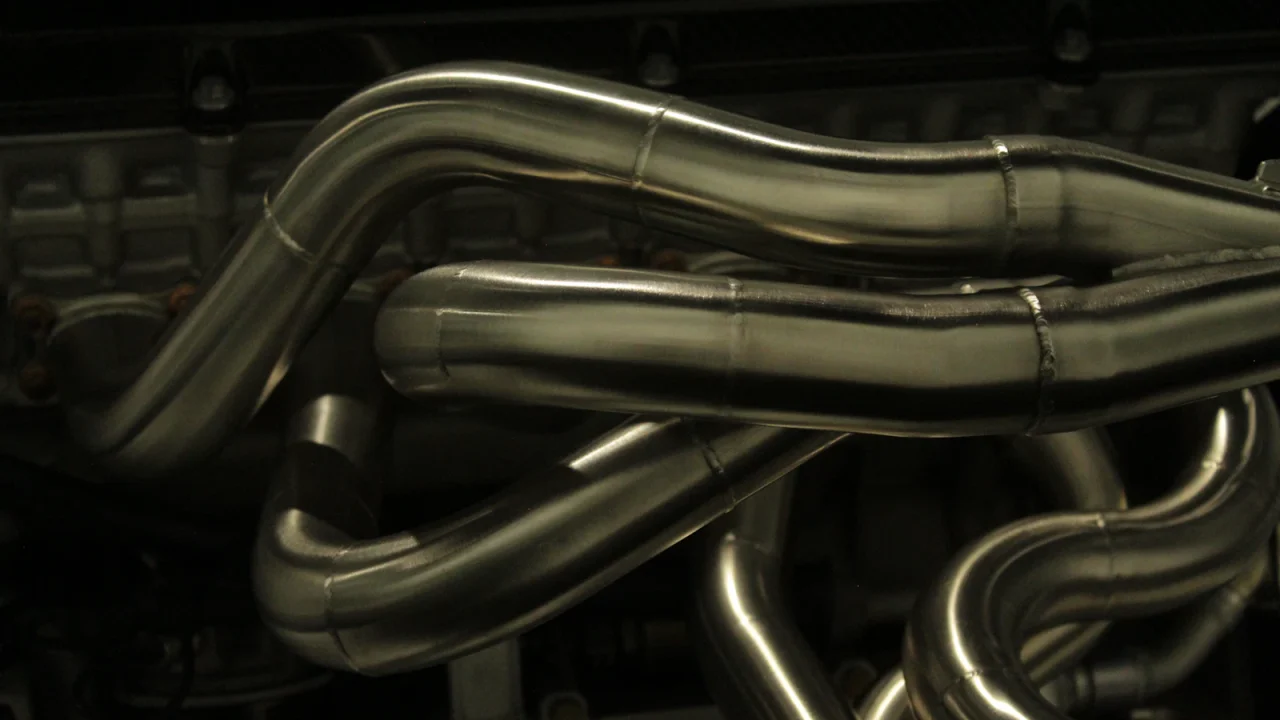
Stainless steel welds with the same processes as mild steel: TIG, MIG and stick. What changes is the filler, the shielding gas and how carefully you manage heat. Match the filler to the grade, keep heat input low, keep carbon steel away from the surface, and control the fumes.
On this page
The fume point is not optional. Welding stainless releases hexavalent chromium, a known cause of lung cancer, so ventilation and respiratory protection need to be planned before the first arc.
Common grades at a basic level
Stainless steel is steel with at least about 10.5% chromium. The chromium forms a thin, self-repairing oxide film that resists rust. Welding well means not damaging that film or the chromium that supports it.
The grades sold for general fabrication are mostly austenitic, the 300 series. They are non-magnetic or only faintly magnetic.
- 304 is the general-purpose grade, with roughly 18% chromium and 8% nickel.
- 316 adds molybdenum for better resistance to salt and chemicals.
- L grades such as 304L and 316L have lower carbon, which helps the weld area keep its corrosion resistance.
Strongly magnetic stainless is usually a ferritic or martensitic 400-series grade. Those behave differently and are outside this guide. If you do not know the grade, ask the supplier.
Process options: TIG, MIG and stick
- TIG gives the most heat control and the cleanest result and suits thin sheet, tube and visible welds. It runs on DC electrode negative. See TIG welding basics.
- MIG is faster and easier on longer joints and thicker material. It needs stainless wire, a different gas, and ideally a liner and drive rolls that have not run carbon steel wire. See MIG welding basics.
- Stick works with stainless electrodes such as E308L-16 and needs no gas. It suits thicker sections, is hard to use on thin material and produces the most fume of the three. See stick welding basics.
The MIG vs TIG vs stick comparison sets out the general trade-offs.
Choosing filler metal
Filler is matched to the base metal. The ER designations below apply to MIG wire and TIG rod. Stick electrodes use the same numbers with an E prefix, such as E308L-16.
| Filler | Use it for | Notes |
|---|---|---|
| ER308L | 304 and 304L to themselves | The standard filler for the most common grade |
| ER316L | 316 and 316L to themselves | Contains molybdenum to match the corrosion resistance of 316 |
| ER309L | Stainless to mild steel | Higher alloy content tolerates dilution from the carbon steel side |
Do not use mild steel filler on stainless. The weld may hold together, but it will rust. A joint between stainless and mild steel will also still rust on the mild steel side unless that side is coated.
Shielding gas
For TIG, use 100% argon.
For MIG, the 75% argon / 25% CO2 mix used on mild steel is the wrong choice. That much CO2 adds carbon to the weld and reduces corrosion resistance. Two common options are:
- Tri-mix, a blend of helium, argon and a small amount of CO2, widely used for short-circuit MIG.
- 98% argon / 2% CO2, another common blend, often used on machines with spray or pulsed modes.
Ask your gas supplier which blend suits your machine and transfer mode, and set flow from the machine’s chart. The MIG welding gas guide explains mixes and flow rates in more detail.
Heat control, distortion and sugaring
Stainless conducts heat more slowly than mild steel and expands more as it warms. Heat stays concentrated near the weld, so thin parts warp. Too much heat for too long also harms corrosion resistance in the zone beside the weld.
- Use the lowest setting that still gives full fusion, and travel steadily without lingering. Charts often list somewhat less amperage than for the same thickness of mild steel. Confirm against your machine’s chart and manual, then test on scrap.
- Run straight stringer beads. Wide weaving adds heat.
- Tack more often than you would on mild steel, and clamp parts firmly.
- Weld in short sections and move around the part instead of running one long bead.
- Let the part cool between passes. A copper or aluminum backing bar clamped behind the joint draws heat away.
Sugaring is the rough, gray, crystalline oxidation that forms on the back of a weld when the root melts through with no gas protecting it. Sugared metal has lost its corrosion resistance and is rough enough to trap dirt.
The fix is back-purging: filling the space behind the joint with argon so the root is shielded too. On tube, that means capping the ends and feeding a low flow of argon inside, with a small vent hole so pressure cannot build up. Where purging is not practical, a tight-fitting backing bar or a weld that does not melt through the full thickness reduces the problem. Argon displaces air, so never purge in an enclosed space without ventilation.
Avoiding contamination and cleaning heat tint
Carbon steel particles embedded in a stainless surface will rust, leaving brown stains that look like the stainless itself is corroding. Keep the two metals apart in your tools:
- Use stainless steel wire brushes that have only ever touched stainless.
- Keep separate flap discs, grinding discs and cut-off wheels, and mark them.
- Do not grind mild steel next to stainless parts. The sparks carry steel particles.
Heat tint is the band of straw, blue or gray color beside a weld. Light straw indicates good heat control. Dark blue and gray mean more heat and a thicker oxide that resists corrosion less well. Remove tint with a dedicated stainless brush or non-woven abrasive. Pickling pastes also remove it, but they contain strong acids and need their own precautions, so read the product safety data sheet before deciding to use one.
Fumes and hexavalent chromium
When stainless is welded, some of the chromium in the fume is converted to hexavalent chromium. NIOSH lists it as harmful to the respiratory system, skin and eyes and links it to lung cancer. Stick welding generally produces the most, and TIG the least, but every process produces some.
- Use local exhaust that captures fume at the arc, such as a fume extractor, and keep your head out of the plume. An open door alone is not enough.
- Wear a respirator rated for welding fume that fits under your helmet, and make sure it seals.
- Treat grinding dust from stainless welds as a hazard too, and clean up with a vacuum instead of compressed air.
The welding safety basics guide covers ventilation in general, and the welding PPE checklist lists the protective gear. This guide covers general fabrication only. Pressure vessels, piping under pressure, fuel tanks and structural parts need qualified welders working to a written procedure.
Frequently asked questions
Can I weld stainless steel with a normal MIG welder?
Can I weld stainless steel to mild steel?
Why did my stainless weld rust?
Is back-purging always necessary?
Sources and further reading
Keep reading
Related guides
Material guide
How to Weld Aluminum: Processes, Prep and Common Problems
Aluminum needs AC TIG or MIG with a spool gun, pure argon and careful cleaning. This guide covers prep, filler choice, technique…
Buying advice
What Welder Should a Beginner Buy?
A beginner should usually buy a wire-feed welder: 120V flux-core for a low-cost start, or a gas-capable MIG machine for cleaner welds…
Material guide
How to Weld Mild Steel: The Beginner’s Material Guide
Mild steel is the easiest metal to learn welding on. This guide covers prep, process choice, wire and rod selection, fit-up, distortion…