Flux-Core Welding Basics: Gasless Welding Explained
Flux-core welding uses a flux-filled wire that shields itself, so no gas is needed; learn polarity, drag technique, slag removal and when it beats MIG.
WelderGuru is reader-supported. As an Amazon Associate we earn from qualifying purchases made through links on this page, at no extra cost to you. Learn more.
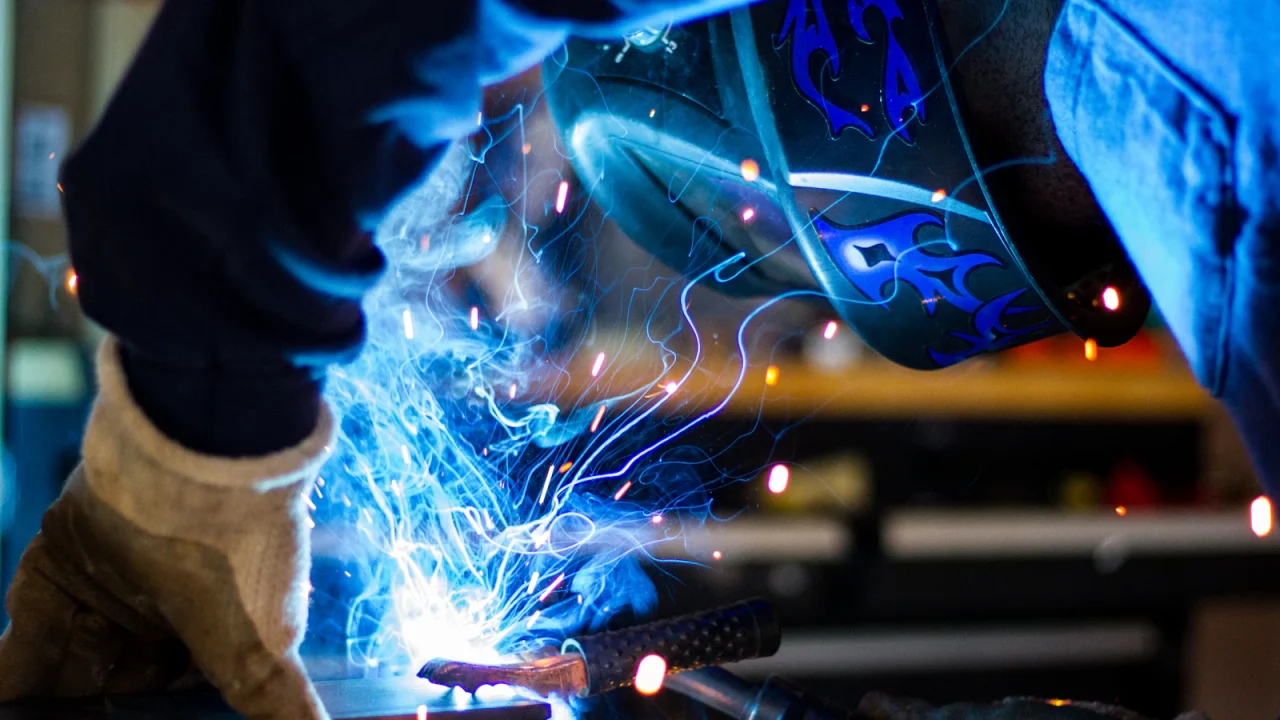
Flux-core welding (FCAW) feeds a hollow wire filled with flux through a MIG-style gun. With self-shielded wire, the flux burns in the arc to make its own shielding gas and a slag cover, so you weld with no gas cylinder. That is what gasless means in practice: the shielding is still there, but it comes from inside the wire.
On this page
It is not MIG with the gas turned off, though. Self-shielded wire usually runs on the opposite polarity, needs knurled drive rolls, wants a longer stickout and a drag technique, and leaves slag to chip. Get those points right and flux-core is a capable process for outdoor work and for thicker or less-than-clean steel.
Self-shielded vs gas-shielded flux-core
| Feature | Self-shielded (FCAW-S) | Gas-shielded (FCAW-G) |
|---|---|---|
| Shielding | From the flux alone, with no cylinder | Flux plus external CO2 or 75/25 argon and CO2 |
| Usual polarity | DCEN (electrode negative) | DCEP (electrode positive) |
| Example wires | E71T-11, E71T-GS | E71T-1 |
| Wind tolerance | Good | Poor, like MIG |
| Where it fits | Home and farm repair with small machines | Fabrication shops with larger machines |
Hobby machines sold as gasless run self-shielded wire, and that is what the rest of this guide covers. E71T-GS is a single-pass wire for thinner material. E71T-11 is a general-purpose wire that can be used for more than one pass within the thickness limits on its data sheet. Gas-shielded wire, often called dual shield, gives smooth welds at high deposition rates but needs a cylinder and more output than small machines provide.
Polarity and machine setup
Most self-shielded wires run on DC electrode negative (DCEN): the gun connects to the negative terminal and the work clamp to the positive. Solid-wire MIG is the reverse. If your machine does both, swap the leads as shown on the diagram inside the wire compartment, and confirm the polarity printed on the wire label. Wrong polarity shows up as heavy spatter, a ropey bead and poor penetration.
- Drive rolls: use knurled V-groove rolls. Cored wire is a soft tube, and smooth rolls either slip or need so much pressure that they crush it.
- Tension: set it just tight enough to feed reliably. Too much flattens the wire and causes tangles at the drive rolls.
- Contact tip: match it to the wire diameter, commonly .030 or .035 inch.
- Voltage and wire speed: start from the chart inside the machine door for your wire and thickness, then confirm against the wire maker’s printed range and the manual.
A 120V machine at full output asks a lot of a household circuit. The power compatibility checker helps you compare a machine’s input needs with your supply, and any new circuit or outlet is a job for a qualified electrician.
Best for beginners
120V flux-core welder
Why consider it
- Runs self-shielded wire from household voltage; check the manual for the circuit rating it requires
- No regulator, hose or cylinder to set up
- Gas-ready types can also run MIG with solid wire if you add a cylinder later
Best for: Home users welding mild steel outdoors or without a gas cylinder
See current options on Amazon (opens Amazon in a new tab)
Type-level recommendation. Compare current models, specifications and prices on Amazon. We may earn a commission.
Technique: drag, stickout and travel speed
Point the gun back at the finished weld and pull it along the joint, at a drag angle of roughly 10 to 20 degrees. Pushing lets slag roll ahead of the arc, where it gets trapped in the weld.
Stickout is longer than with MIG. Short-circuit MIG runs about 3/8 inch, while small self-shielded wires commonly call for around 1/2 to 3/4 inch from contact tip to work. The correct figure is on the wire data sheet. Hold it steady, because stickout changes the heat reaching the puddle.
Keep the arc on the leading edge of the puddle and travel fast enough to stay ahead of the slag. On thin sheet, flux-core runs hot and burns through easily. For that work, solid wire with gas is the better choice, as the MIG vs flux-core comparison explains.
Slag, spatter and fume
Slag. Every flux-core weld is covered in slag. Chip it and wire-brush the bead before you weld over or next to it, or the slag ends up inside the joint.
Spatter. Expect more than MIG. Correct polarity, the right voltage and a steady stickout keep it manageable, and anti-spatter spray makes cleanup easier. The spatter troubleshooting guide covers the causes.
Porosity. Damp wire, too much voltage and the wrong stickout cause pinholes and worm tracks on the bead surface. Store wire dry and see the porosity guide if they appear.
Fume. Flux-core makes noticeably more fume than solid wire. Keep your head out of the plume and weld with good ventilation. Remove galvanizing, paint and other coatings from the weld area first, because heated coatings add hazardous fume. The welding safety basics guide covers fume control.
Where flux-core beats MIG
Strengths
- No gas cylinder to buy, refill or carry
- Shielding holds up in wind, so it works outdoors
- Good penetration on thicker steel from a small machine
- More tolerant of light rust and mill scale than solid wire
Limitations
- More spatter and fume than MIG
- Slag must be chipped off every pass
- Burns through thin sheet metal easily
- Rougher bead that needs more cleanup
Choose flux-core for non-structural repairs done outside, such as gates, brackets and garden equipment, and for steel around 1/8 inch and thicker when you only have a small machine. Choose MIG for thin sheet and clean indoor fabrication where appearance matters. Gas-ready machines run both, so you can start gasless and add a cylinder later. MIG welding basics covers that side, and the flux-core welder buying guide covers machine types.
Frequently asked questions
Do I need gas for flux-core welding?
What polarity should I use for flux-core?
Can I run flux-core wire in a MIG welder?
Why do my flux-core welds look rough and full of holes?
Can flux-core weld thin sheet metal?
Sources and further reading
Keep reading
Related guides
Material guide
How to Weld Aluminum: Processes, Prep and Common Problems
Aluminum needs AC TIG or MIG with a spool gun, pure argon and careful cleaning. This guide covers prep, filler choice, technique…
Buying advice
What Welder Should a Beginner Buy?
A beginner should usually buy a wire-feed welder: 120V flux-core for a low-cost start, or a gas-capable MIG machine for cleaner welds…
Material guide
How to Weld Mild Steel: The Beginner’s Material Guide
Mild steel is the easiest metal to learn welding on. This guide covers prep, process choice, wire and rod selection, fit-up, distortion…